
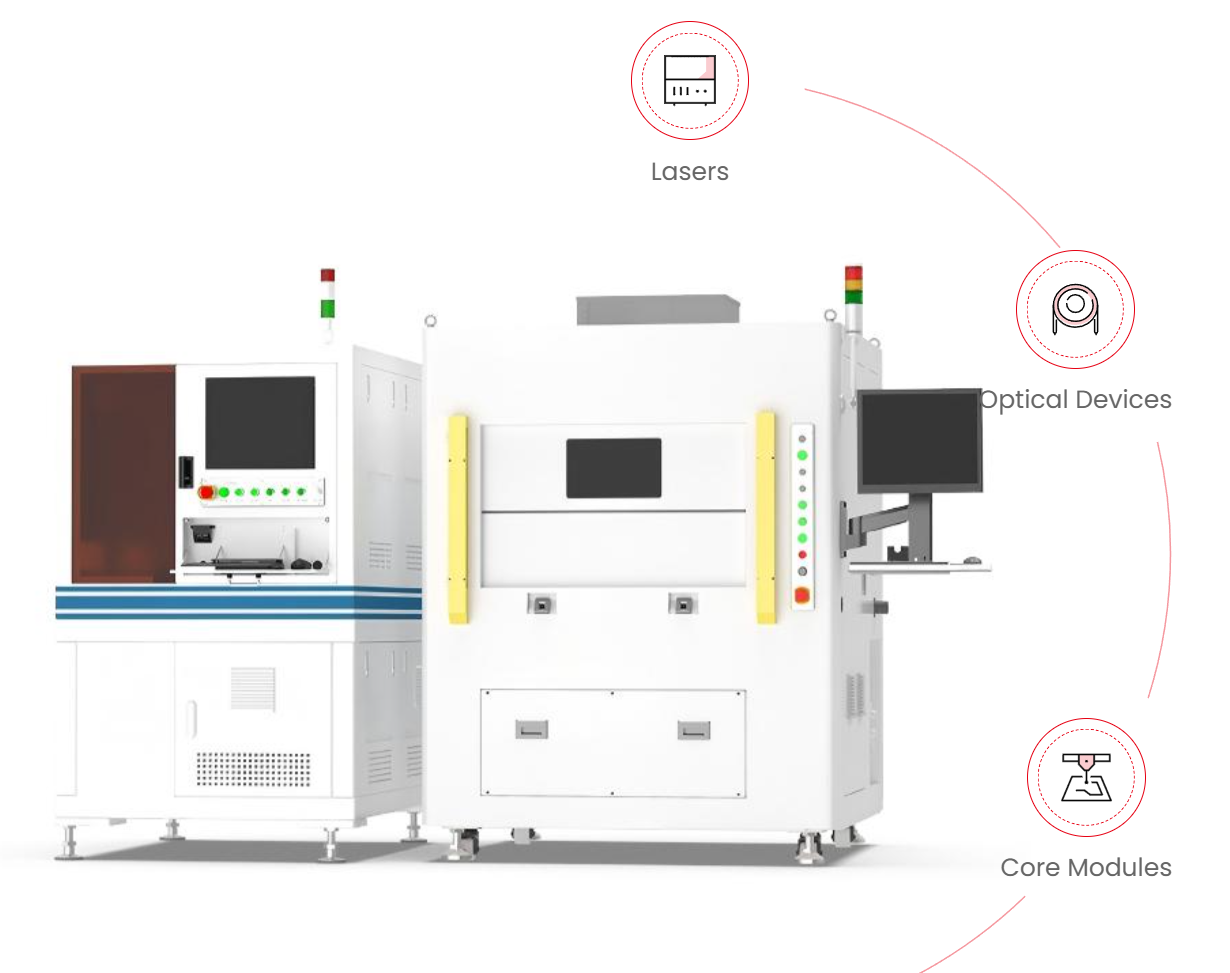
Framework overview: why a disciplined approach matters
Integrating laser cleaning into a multi-axis CNC line calls for a repeatable framework that balances process control, safety, and uptime. Start by acknowledging the laser modality — for many industrial cleaning tasks, a qcw laser or similar source will be considered for its pulse shaping and average power characteristics — then map how that source interfaces with motion control, fixtures, and the shop’s QA gates. The 2020 global supply-chain disruptions and pressures on Detroit-area OEMs made one thing clear: ad hoc installs create hidden failure modes. A structured checklist prevents those surprises.
Step 1 — Define the cleaning outcomes and constraints
Begin with measurable acceptance criteria: residue limits, surface roughness thresholds, allowable heat input, and cycle time per part. Identify substrates (aluminum, stainless, composite) and contaminants (oxides, coatings, adhesives). Record existing cycle times on the CNC and target throughput; this frames laser power and motion requirements. Include one or two industry terms in your spec — e.g., desired beam profile and maximum acceptable focal length variation — so integrators and OEMs speak the same language.
Step 2 — Select the laser and optics to fit the workflow
Match the laser type to the application: pulsed QCW or CW fiber sources each have strengths. For fine oxide removal with minimal substrate heating, short pulses and controlled duty cycles help. For broad, rapid stripping on thick coatings, higher average power from cw fiber lasers may be appropriate. Consider scan head size, beam-homogenization needs, and the wavelength’s absorption on your material. These specifics affect cycle time, required focal lengths, and the choice of beam delivery (fiber vs free-space).
Step 3 — Motion integration and fixture strategy
Integrate the laser with the CNC’s kinematics so beam incidence and standoff remain consistent. Decide whether to mount the scanner on the spindle, keep it fixed at a secondary station, or use an articulated arm. For multi-axis paths, coordinate galvo scan patterns with axis motion to avoid over- or under-exposure. Fixtures should index repeatably; small clamping variation changes focal distance and can alter results. Don’t ignore interlocks and safety zones — those are part of the cycle time calculation too.
Step 4 — Controls, synchronization, and communication
Ensure the laser controller can accept real-time triggers or an IEC-style fieldbus from your CNC. Define handshake sequences: ready-to-fire, inhibit, and fault clear. If you need synchronized motion with a scan head, verify latency and jitter specifications — they matter when spot overlap is critical. Also consider logging: timestamped beam-on events, power meters, and process cameras help with traceability and root-cause analysis later.
Step 5 — Safety, extraction, and environmental controls
Laser safety isn’t optional. Enclose beam paths where practical, implement interlocks, and define PPE and eyewear rules. Plan fume extraction and filtration because ablated material can be harmful; match the extraction flow to the process’s particulate and vapor load. Temperature control is often overlooked: ambient and part temperature affect absorption and may require air knives or localized cooling to stay within thermal budgets.
Step 6 — Commissioning, qualification, and feedback loops
Run qualification trials using production fixtures and parts. Capture data on laser power stability, cycle time variance, and part rework rates. Define clear first-article acceptance criteria and automate tests where possible. In many installations — I’ve seen this in Midwest machine shops supplying automotive tiers — a short validation stage caught misaligned focus and prevented costly rework on full production runs. This real-world anchor reminds us that the smallest setup errors compound quickly on volume lines.
Common mistakes and how to avoid them
Teams commonly under-spec the beam delivery tolerance, ignore mounting-induced drift, or treat safety as an afterthought. They also sometimes expect the laser to mimic chemical cleaning without adjusting exposure maps — you’ll overshoot the substrate if you don’t compensate. A good mitigation plan: document tolerances, schedule thermal-cycle checks, and insist on a trial run with a full production cassette — those early checks often save weeks on the back end. —
Integration trade-offs: cost, speed, and quality
There are always trade-offs. Lower-cost laser heads can meet throughput on softer substrates but may struggle with consistent beam profiles over long runs. High-end scan heads and power-stabilized sources offer repeatability but raise upfront capital. Decide whether you value lower unit cost or lower scrap rates more — that informs whether to invest in beam homogenizers, closed-loop power control, or advanced optics with longer focal lengths for reliability across part geometries.
Vendor selection and in-factory support
Pick vendors who provide more than hardware: look for application support, on-site commissioning, and documentation for process control. Check for field-proven case studies in similar industries and verify service response times. Ask about spares, mean time to repair, and software update policies. Integration often fails from poor support, not from the laser’s basic capabilities.
Summary of the framework
Start with clear acceptance criteria, choose laser and optics to match the substrate and throughput, integrate motion and controls tightly, address safety and extraction up front, and run rigorous qualification trials. These steps reduce surprises and shorten time-to-stable-production — and they let you scale without repeatedly revisiting the basics.
Advisory: three critical evaluation metrics
1) Process repeatability: measure parts-per-million defects over a defined production window and insist on supplier data for beam power stability and positioning jitter. 2) Integration latency: verify control-loop latencies between CNC and laser to ensure synchronized exposure, especially where galvo scanning and axis motion coincide. 3) Total cost of ownership: include downtime risk, spare-part lead times, and extraction/ventilation investments when comparing bids.
For practical installs, reliability in hardware and clarity in procedures are what keep production lines humming — and many teams find that a partner who understands both laser physics and shop-floor realities provides the most durable solution. JPT. —