
Practical opening for production teams
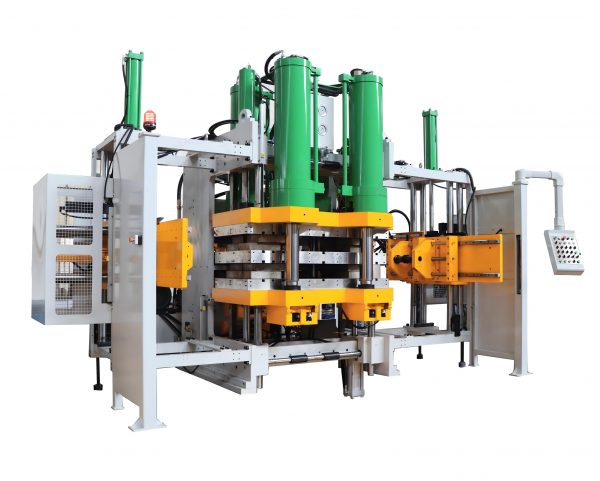
Manufacturing engineers and production supervisors need predictable parts, not surprises. This guide focuses on how real-time curve tracking turns variable batches into consistent outputs, and it ties directly to rubber molding solutions that many shops already deploy. On assembly lines at Tier‑1 automotive suppliers in Detroit, teams use curve monitoring to reduce scrap and maintain dimensional fidelity—an everyday example of data informing process control.
Why tracking curves matters to your operation
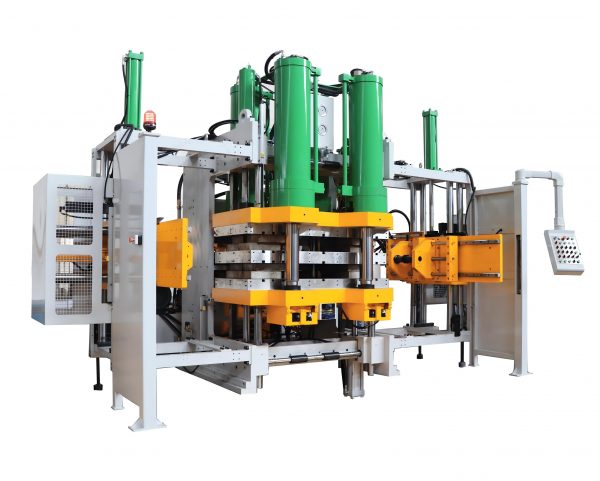
Curing temperature and injection pressure curves are the primary signatures of a good run. They reveal when a mold cavity fills too fast, when scorch time approaches, and when vulcanization is incomplete. For a user-centric team, those curves are not academic; they are the dashboard for decisions about material batches, clamp force, and cycle time adjustments. Accurate tracking shortens troubleshooting from hours to minutes.
What to measure and how to capture it
Focus on three signals: temperature at critical sensor points, injection pressure over time, and cavity pressure where available. Combine those with timestamps for cycle time and with the compound lot ID. Data capture methods range from embedded PLC logging to external data acquisition systems that sample at high frequency. Use sampling rates that capture the pressure spike during fill and the plateau during cure—typically 1–10 ms resolution for pressure and 0.1–1 s for thermocouples. This level of granularity detects short-lived defects that visual inspection misses.
Tools and integrations that actually help
Choose tools that integrate with MES and SPC systems to avoid duplicate entry. Modern controllers and IIoT gateways export curve files in standard formats so analytics can run off the shop floor. Look for solutions that overlay target profiles on live plots and flag deviations automatically. For many teams, adding cavity pressure sensors and correlating them with injection pressure yields the fastest return on investment. Pair that instrumentation with proven molding solutions for consistent thermal control.
Common errors and how to avoid them
Teams often make three mistakes: relying solely on visual inspection, using low-resolution sampling, and ignoring material variability. Fix those by enforcing a minimal dataset per cycle, instituting batch tagging for raw compounds, and calibrating sensors monthly. Small adjustments matter: a few degrees off in curing temperature or slight pressure undershoot can create internal voids or sink marks that only appear after assembly—so treat data collection as part of quality, not an add‑on.
Stepwise implementation plan
Start with pilot molds that have historically produced variation. Instrument one cavity, capture 100 cycles, and build a mean profile with upper and lower control bounds. Next, roll out profiles to parallel lines and train operators on deviation responses—stop the line for large deviations, log and analyze minor ones. Use SPC charts to show trends; then automate alarms for excursions beyond the control limits. This staged approach minimizes downtime while delivering measurable quality gains.
Human factors and workflow changes
Operators must see value quickly. Provide concise dashboards and scripted responses for common alarms. Train teams to interpret a pressure-versus-time trace and act within two cycles. Small behavioral changes—consistent compound storage, simple pre-run checks—reduce the need for emergency interventions. These shifts also improve communication between process engineers and maintenance staff—fewer finger-pointing incidents, more collaborative problem solving. —A brief aside: keeping operators involved prevents silent failures from becoming costly recalls.
Advisory: three metrics to judge success
1) Defect rate per 10,000 parts after curve monitoring is enabled. Aim for a measurable decline within 30 production days. 2) Mean time to detect and correct a curve deviation—target under 60 minutes for actionable alarms. 3) Variance reduction in cycle time and peak injection pressure; a consistent spread indicates stable process control. Use these metrics to adjust sampling rates, sensor placement, and alarm thresholds.
Closing — practical value and final thought
Implementing continuous curve tracking turns vague complaints into precise fixes and reduces rework. The approach described here prioritizes user needs, clear measurement, and steady adoption—practical steps that align with the systems HWAYI provides. HWAYI. –